头部背景图片

Reciprocating Pumps Dominate High-Pressure Cementing Operations

2026-05-22

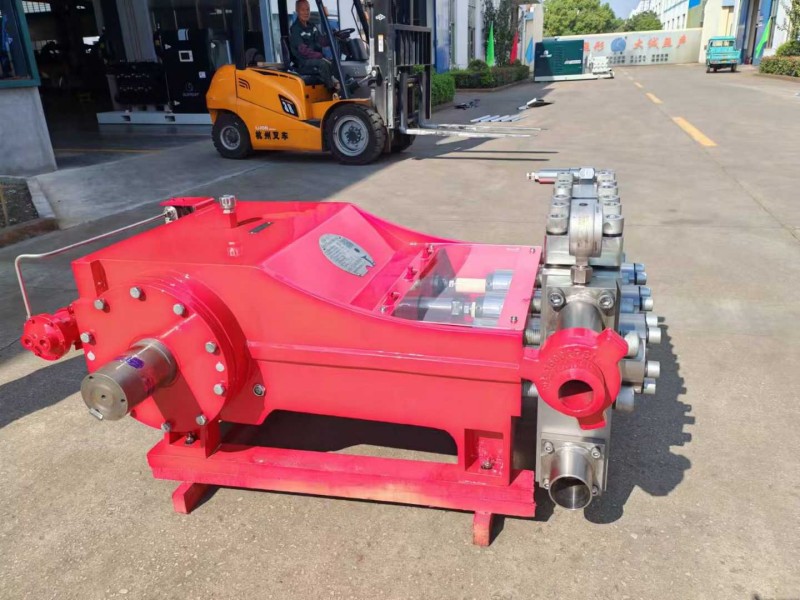
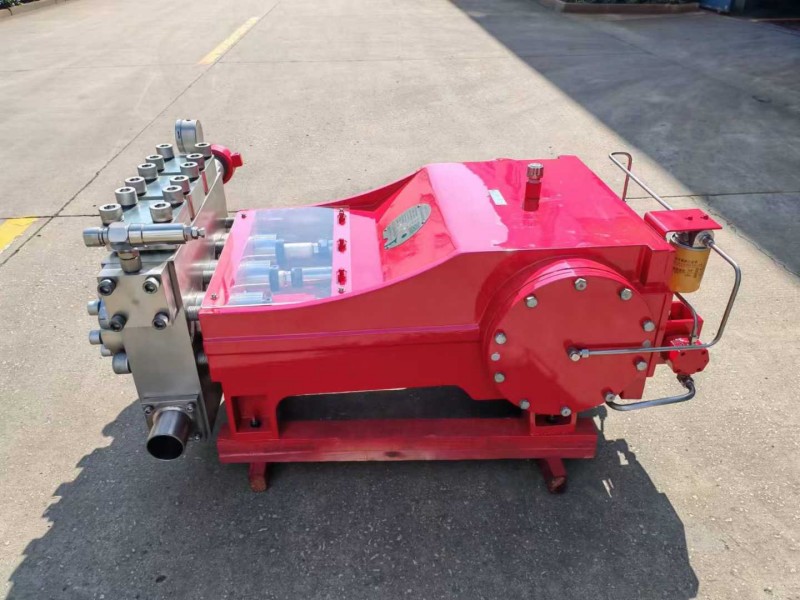
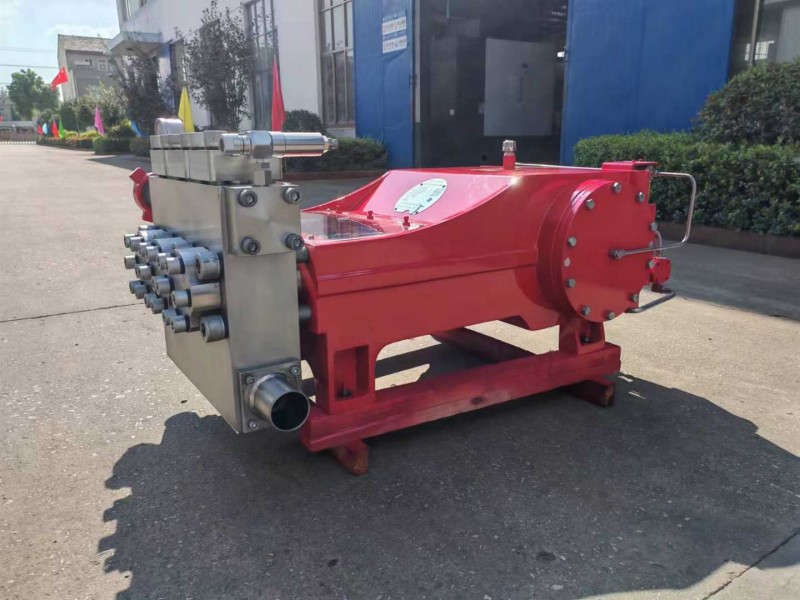
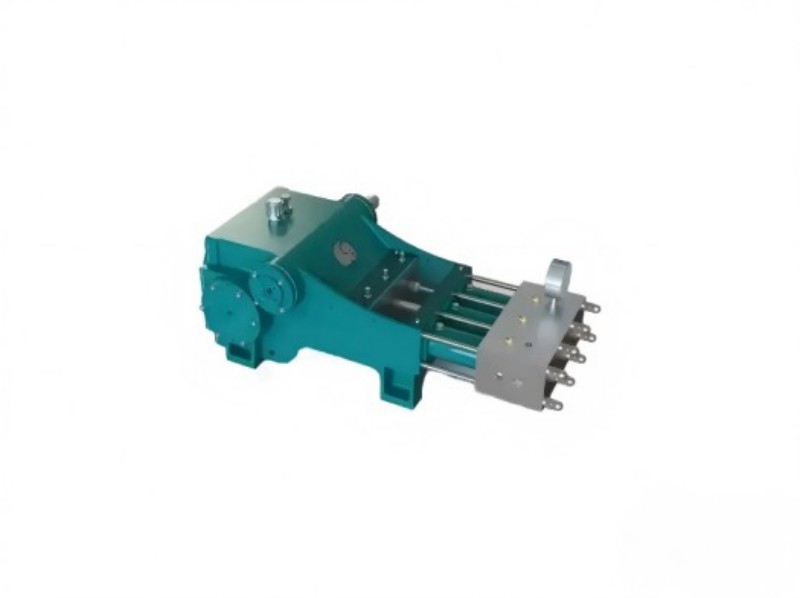
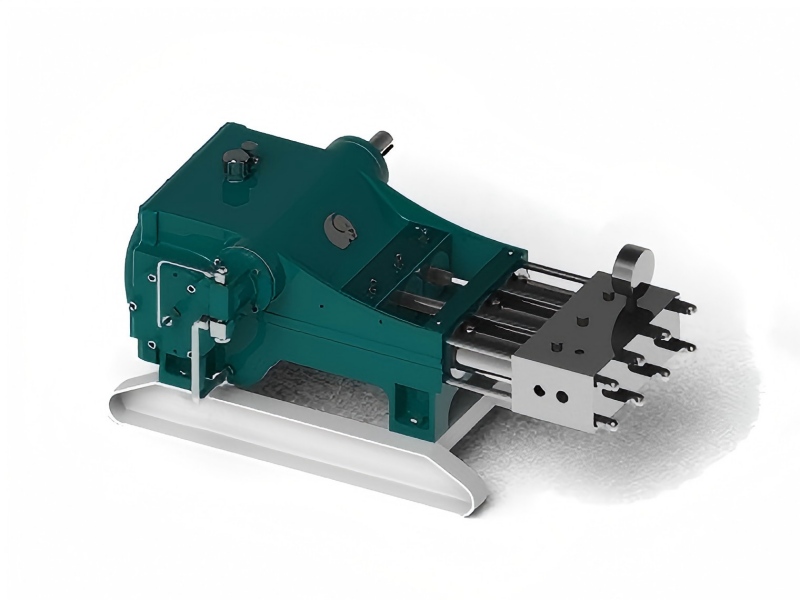
In the field of oil drilling, cementing operations are a critical process for ensuring wellbore stability and sealing off oil, gas, and water zones, directly impacting well construction safety and production lifespan. Pumping high-pressure cement slurry is at the core of cementing operations, and reciprocating plunger pumps dominate the market due to their performance advantages.


1. Advantages of Reciprocating Pumps

They offer a wide pressure adjustment range, making them suitable for drilling operations at various depths and under different conditions, and can operate stably even in ultra-deep wells under high-pressure conditions. They exhibit strong adaptability to media, as cement slurry contains solid particles and varies significantly in viscosity. They provide high flow rate control precision, enabling accurate regulation according to operational requirements.


2. Technical Features

Maintenance and repairs are convenient, allowing for quick replacement of wear-prone components, which reduces downtime and improves construction efficiency. Furthermore, the pump’s pressure control technology is mature and can be equipped with an intelligent pump station system to monitor and dynamically adjust pressure in real time, enhancing construction safety.


3. Reliability

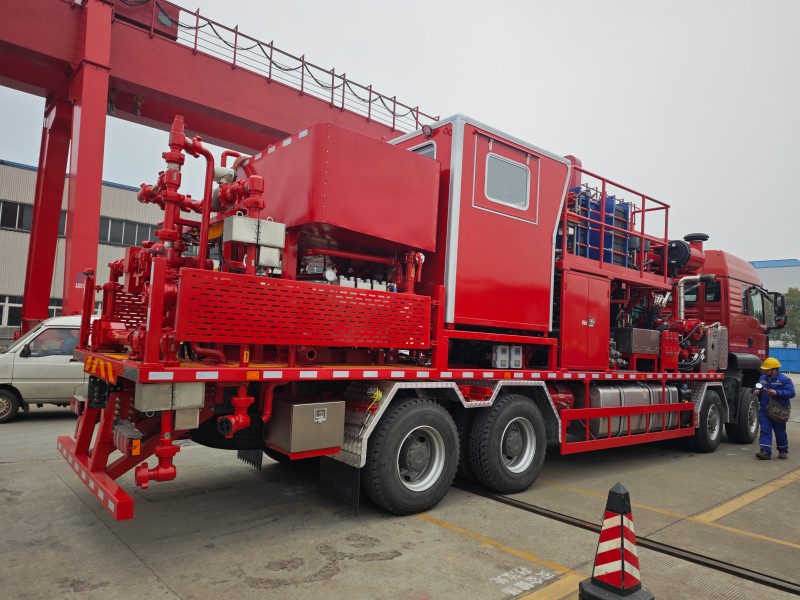
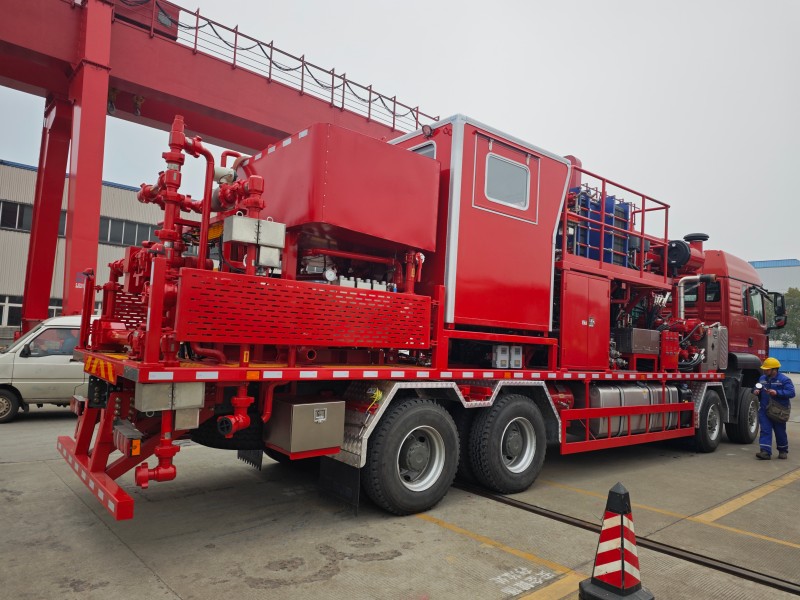
Components undergo wear-resistant hardening treatment to extend the service life of wear-prone parts, meeting the requirements of long-term continuous pumping during cementing operations. The pump’s power transmission system offers excellent compatibility and high power conversion efficiency. Energy consumption remains stable during high-pressure, high-flow operations. It can be installed and deployed in various operational scenarios, such as on-board vehicles and fixed pump stations, further adapting to diverse cementing site environments.


4. Pump Model Selection

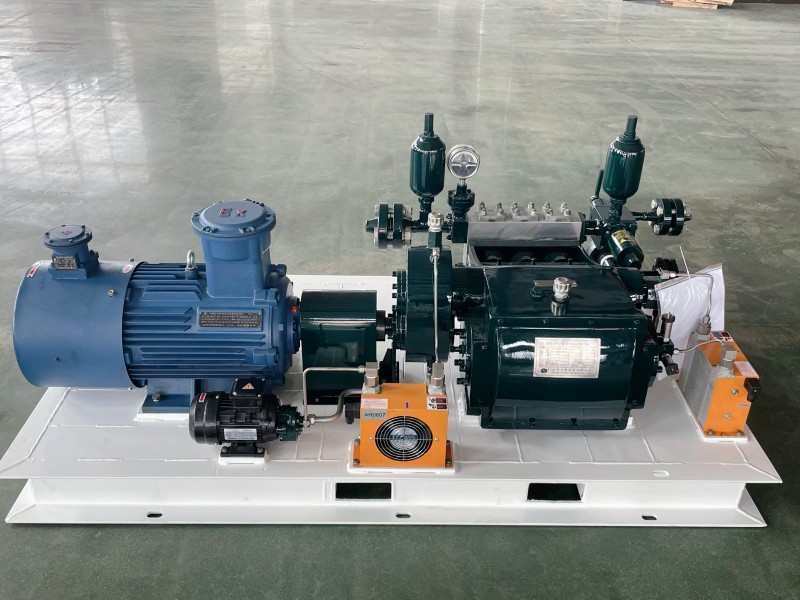
Triplex pump: The most widely used model, featuring low output pulsation and high operational stability.

Quintuplex pump: Suitable for operations with stringent stability and precision requirements, offering minimal fluctuations in output pressure.


In today’s energy industry, where efficiency and safety are paramount, reciprocating plunger pumps are at the heart of cementing equipment. Elephant Machinery is committed to adhering to API 674 standards and utilizing advanced manufacturing processes to provide more convenient, reliable, efficient, and intelligent pumping solutions for oil and gas fields worldwide. 

The Benefits of Skid-Mounted Pressure Test Systems

2026-05-22

Pressure test is a critical step in ensuring the safety of pipelines and pressure vessels, and is commonly used in the oil and gas, mining, trenchless construction, and large-scale water treatment industries.


1. What Is a Skid-Mounted Pressure Test System?

A skid-mounted pressure test system is an integrated unit in which all core functional components required for pressure testing—including pump sets, control units, pressure boosters, pressure sensors, safety protection components, and pipeline valves—are integrated and mounted on a single skid-mounted base. Unlike traditional, piecemeal pressure testing equipment, all components are pre-integrated and pre-commissioned. The entire unit can be quickly transported via crane or trailer, eliminating the need for complex on-site installation, calibration, and commissioning. Upon arrival at the site, it can be rapidly connected to the pipeline or vessel under test to begin operations, making it a fully integrated, mobile pressure testing system.


2. Advantages of Skid-Mounted Pressure Test Systems

• Higher operational efficiency. Compared to traditional pressure testing, skid-mounted pressure testing systems are fully integrated and commissioned before leaving the factory. On-site, testing can begin immediately after connecting to the test object and performing a simple inspection, significantly reducing preparation time.

• Greater flexibility in installation and transportation. The entire system is integrated onto a single skid-mounted base, featuring a compact design with weight and dimensions that meet standard transportation requirements, making it adaptable to various operational scenarios.

• Enhanced stability and safety. Unified commissioning and calibration ensure the accuracy of test data.

• More convenient maintenance and management. Issues can be quickly identified and resolved, reducing operational and maintenance complexity and costs.


Scaffold-mounted pressure test systems offer significant improvements in efficiency, adaptability, reliability, and operational costs, making them ideal for pressure testing scenarios that require rapid deployment and flexible relocation. Elephant Machinery can provide further technical details regarding triplex plunger and quintuplex plunger reciprocating pumps. Please feel free to contact us at any time!

What is a well killing pump?

2026-05-22

A well killing pump is a special high pressure pump used in the oil and gas industry. Its main function is to inject well killing fluid into the well during the well killing operation, balancing the bottomhole formation pressure and ensuring the safety of downhole operations.


1. Operating Principle

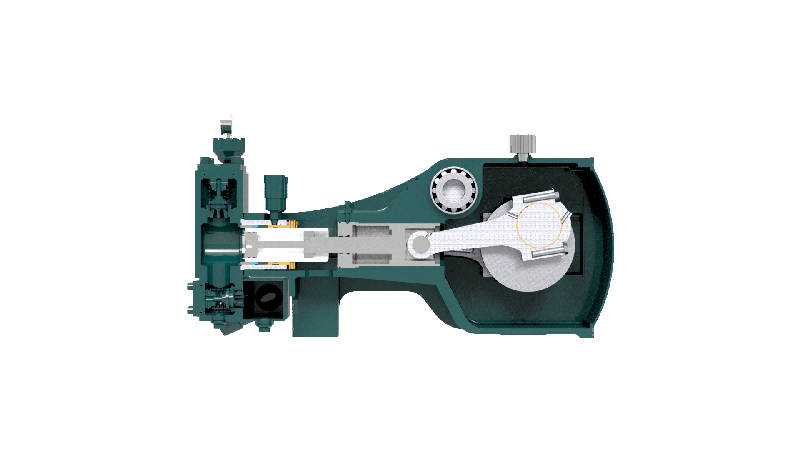
Triplex and quintuplex reciprocating plunger pumps are commonly used as well control pumps. The pump is driven by a power unit that rotates the crankshaft and connects to the connecting rod mechanism, causing the plunger to move in a reciprocating linear motion. When the plunger moves backward, the volume of the pump chamber increases, creating a vacuum; the suction valve opens, allowing the well-control fluid to enter the pump chamber. When the plunger moves forward, the volume of the pump chamber decreases and pressure rises; the discharge valve opens, and high pressure well-control fluid is pumped out and injected into the wellbore. This process ensures a continuous, stable high pressure output, meeting the requirements of well-control operations for high pressure, high-flow-rate injection.


2. Why Reciprocating Pumps Are Preferred
Well killing operations require stable, high pressure output that can be precisely controlled. Reciprocating plunger pumps offer high volumetric efficiency, and their output pressure is minimally affected by load variations, enabling them to maintain working pressure under different operating conditions. Additionally, their displacement can be flexibly adjusted as needed, making them suitable for well killing operations in oil and gas wells of varying depths and pressure levels—fully meeting the operational requirements of the well killing process.


3. Application

In addition to being used in well killing operations for oil and gas wells, the well killing pump can also be used in circulation well killing and squeeze cementing operations during drilling and workover, as well as in high pressure construction scenarios such as high pressure water injection and acid fracturing in the later stages of oil and gas field development.


The well killing pump is a key safety safeguard in oilfield operations and one of the core equipment ensuring downhole operational safety. Elephant Machinery specializes in the R&D and manufacturing of high-quality industrial reciprocating pumps. If you have any requirements for well killing pump selection or customization, please feel free to contact our technical team!

Why Reciprocating Pumps Excel in High Pressure Boiler Feed

2026-05-22

In high pressure boiler feed systems, there are extremely high requirements for the pressure-bearing capacity and output stability of the pumping equipment, and the characteristics of reciprocating pumps are ideally suited to meet these demands.


1. Stability

Reciprocating pumps generate power through the reciprocating motion of pistons or plungers. As long as the power source and pump housing are sufficiently robust, they can maintain high pressure consistently over the long term. Furthermore, since flow rate depends on the plunger stroke and reciprocating frequency, it remains relatively stable and is not affected by fluctuations in boiler operating conditions or changes in feed resistance, thereby ensuring stable feed supply.


2. High Pressure Output Capacity

The sealing structure between the plunger and the pump cylinder in a reciprocating pump can be adjusted to accommodate high pressure operating conditions. It is capable of withstanding extremely high feed pressures, effectively preventing the seal failure and increased internal leakage that often occur in rotary pumps—such as centrifugal pumps—under high pressure conditions. Furthermore, its output capacity does not decrease significantly with rising pressure, ensuring it can consistently meet the feed pressure requirements of high pressure boilers.


3. High Efficiency

Reciprocating pumps generate power by directly compressing the fluid with a plunger, resulting in fewer energy transfer steps and higher conversion efficiency. Additionally, they can flexibly adjust the stroke or reciprocation frequency to precisely control flow rate according to boiler feed requirements.


4. Accuracy

The output flow rate of a reciprocating pump depends on the plunger stroke and stroke frequency, with a clear correlation between these parameters. This eliminates the flow rate deviations caused by pressure and operating condition fluctuations that are common in other pump types. When combined with an intelligent control system, reciprocating pumps can precisely adjust output parameters to match the boiler’s real-time feed requirements, ensuring safe boiler operation.


The outstanding performance of reciprocating pumps in high pressure boiler feed systems stems from the high pressure output, stable flow characteristics, and high efficiency inherent in their positive displacement operating principle. Elephant Machinery’s reciprocating pumps are renowned for their convenient, reliable, efficient, and intelligent, making them the perfect fit for a wide range of operating conditions!

Are Forged Wheels Worth the Investment for Daily Drivers?

2026-05-22

Forged wheels are often associated with race cars, luxury vehicles, and high-performance builds. But many car owners have a more practical question: are forged wheels really worth it for daily driving?

The answer depends on what you expect from your wheels. If you only need a basic replacement wheel, a standard cast wheel may be enough. But if you care about strength, weight, fitment, and a cleaner custom look, forged wheels can be a meaningful upgrade even for a daily driver.


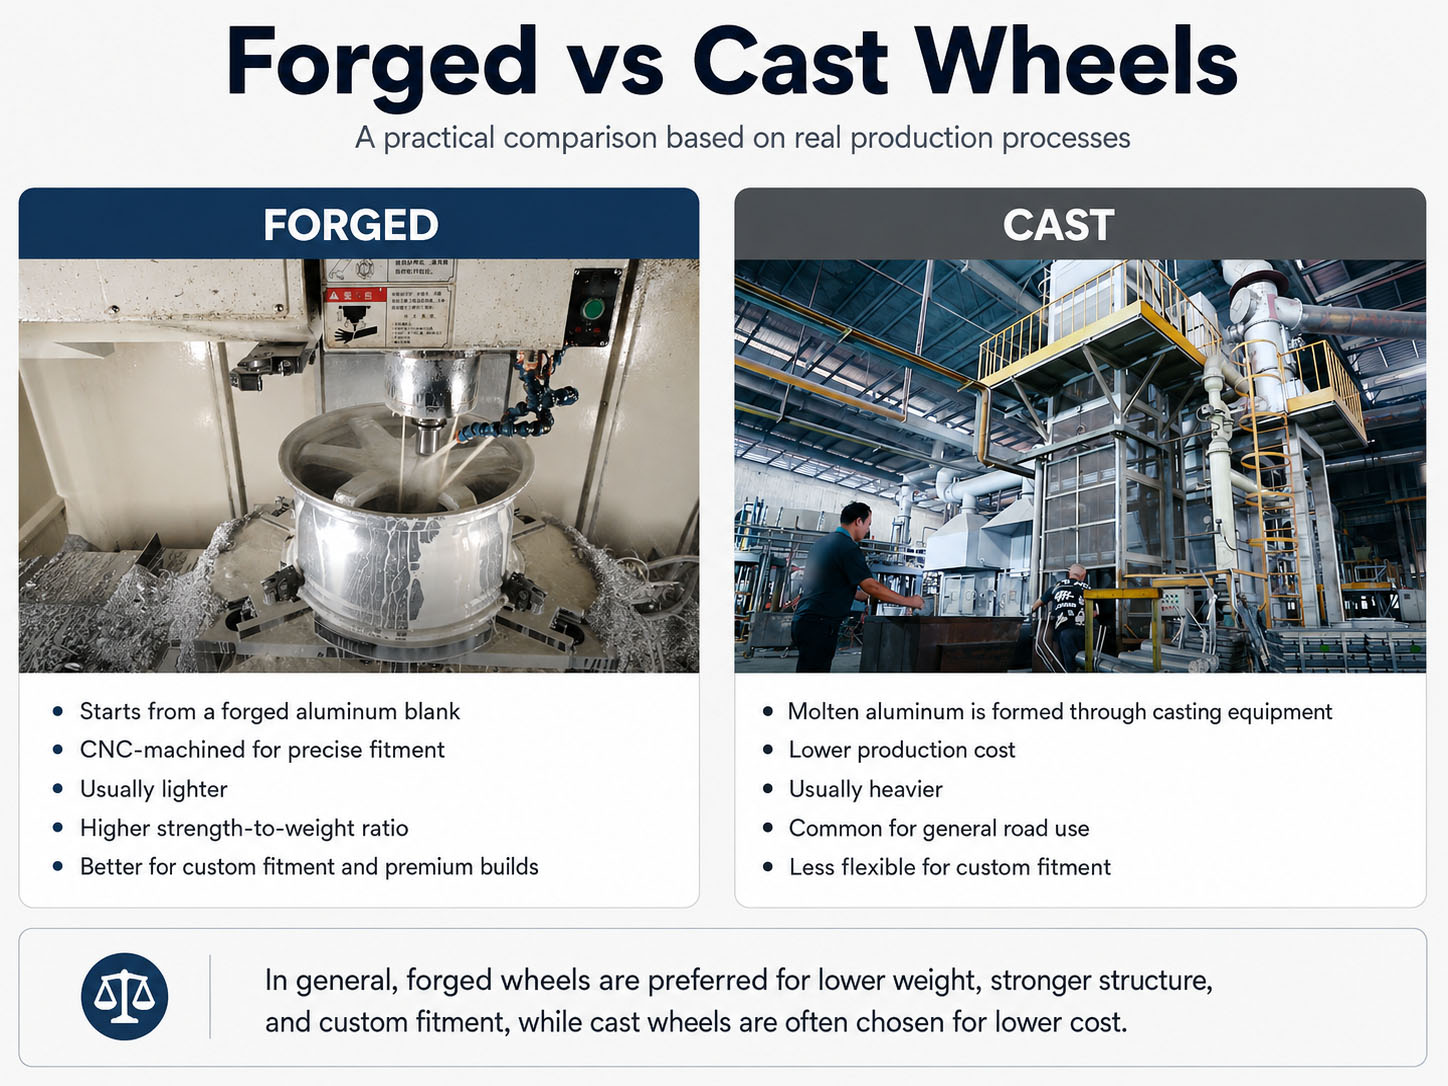
A forged wheel is made by applying high pressure to a solid piece of aluminum, rather than pouring molten aluminum into a mold like a cast wheel. This process helps create a denser and stronger wheel structure. For daily use, that strength matters. City roads, potholes, speed bumps, rough pavement, and unexpected impacts are all part of normal driving. A well-made forged aluminum wheel can offer better durability while keeping the wheel weight lower than many cast alternatives.


Cast vs forged wheels manufacturing comparison

Weight is one of the biggest reasons drivers choose forged wheels. Lighter wheels reduce unsprung weight, which may help the suspension respond more efficiently. In real driving, this can contribute to sharper steering feel and a more responsive driving experience. The difference may not turn a daily car into a track car, but it can make the vehicle feel more refined, especially on premium sedans, SUVs, and performance models.


Another important benefit is fitment. Custom forged wheels can be made according to the vehicle’s specifications, including diameter, width, offset, bolt pattern, and brake clearance. This is especially useful for owners who want a flush stance without relying on spacers or unsuitable factory sizes. For example, many customers choose 19 inch forged wheels or 20 inch forged wheels to improve the appearance of the car while still keeping daily comfort in mind.


Appearance is also part of the value. Forged wheels are highly customizable, from spoke design to surface finish. Options such as brushed, polished, matte black, bronze, gunmetal, and two-tone finishes allow the wheel to match the style of the car. For daily drivers, this means the upgrade is not only about performance, but also about making the vehicle look more personal and premium.

Of course, forged wheels cost more than cast wheels. That is the main reason some drivers hesitate. But the higher price also reflects the material, manufacturing process, engineering work, and customization involved. If you plan to keep your vehicle for several years, or if you are building a car with specific fitment and style requirements, forged wheels can be a long-term investment rather than just a cosmetic upgrade.


So, are forged wheels worth it for daily drivers? For owners who want the lowest-cost option, they may not be necessary. But for those who value lightweight performance, stronger construction, accurate fitment, and a custom appearance, forged wheels are definitely worth considering.

At Rimpower, we manufacture custom forged wheels using T6061-T6 aluminum, with fitment support for luxury cars, SUVs, and performance vehicles. Each order can be customized based on your vehicle data, design preference, and finish requirements.


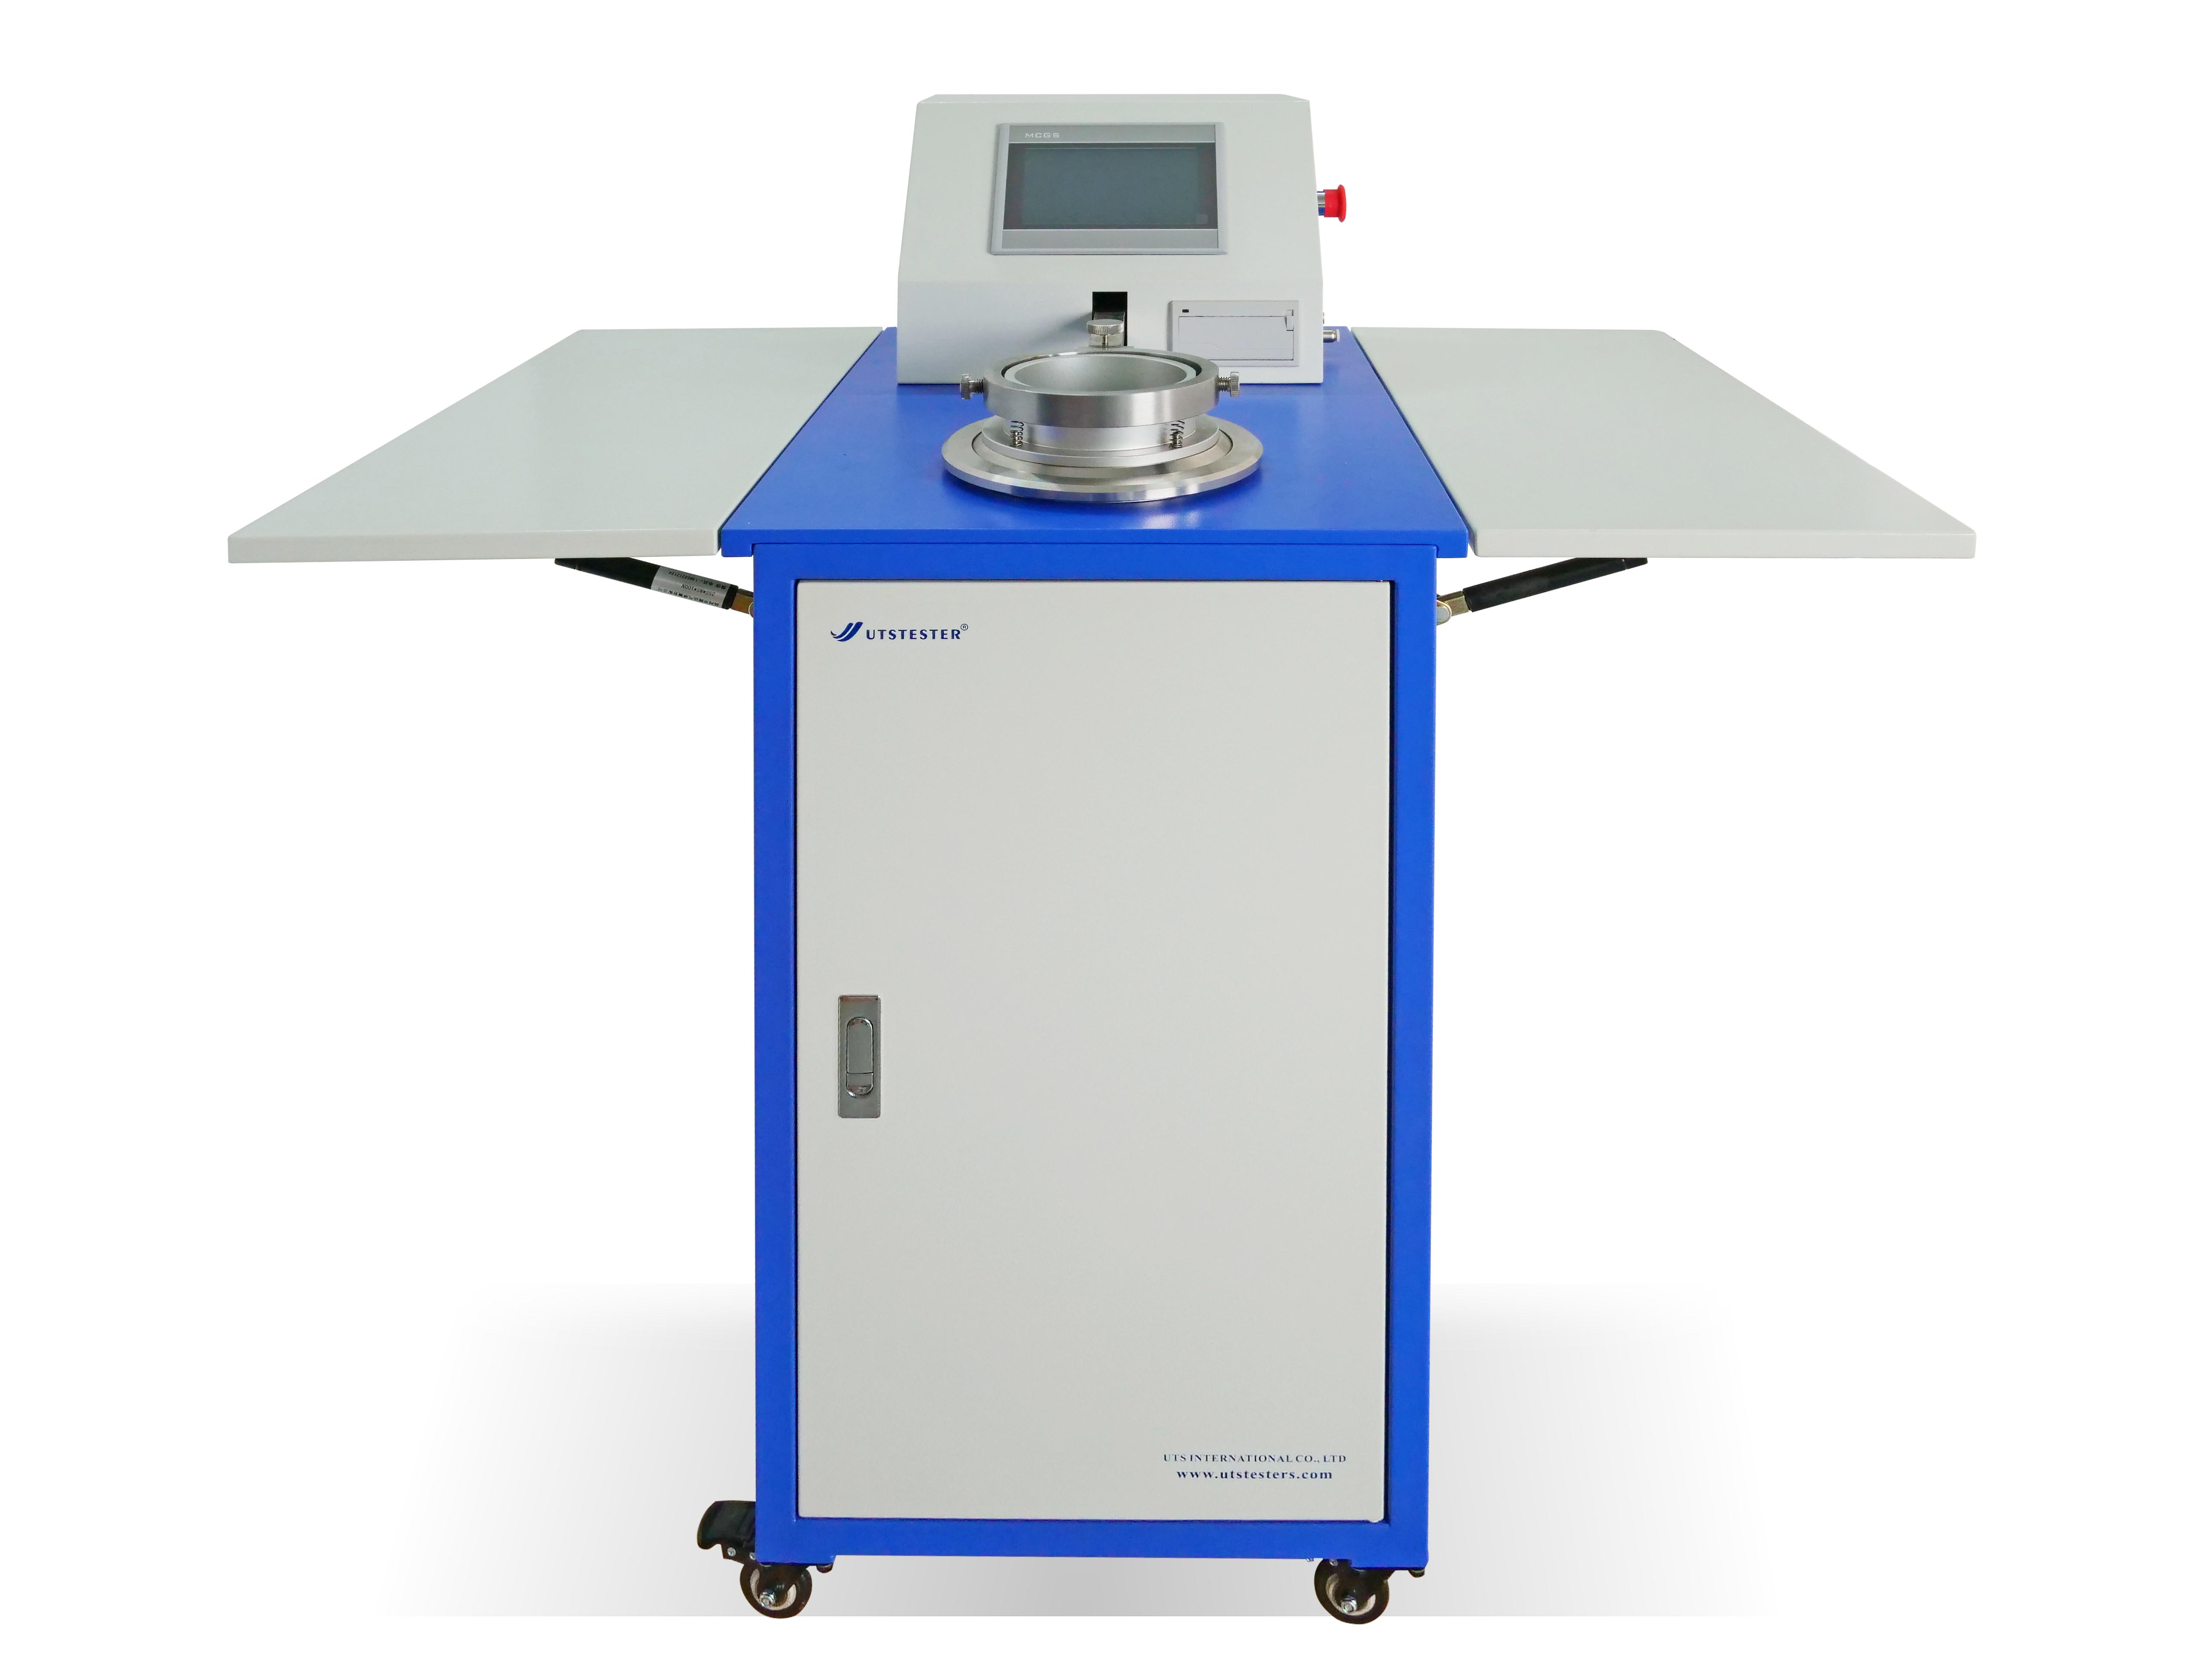
Fabric air permeability tester

2026-05-15

The significance of fabric air permeability test


Air permeability is a physical index that characterizes the air permeability in the tested sample, mainly for porous materials with large air permeability, such as textiles, sponges, leather, etc. For fabric materials, the air permeability is related to the number and size of the gaps between the warp and weft yarns and the gaps between the fibers, the warp and weft density, the yarn twist, the fiber properties, the yarn structure, the fabric thickness and other factors.Different requirements for fabrics have different air permeability according to their specific uses. For example, the air permeability of fabrics used to make parachutes should be strictly controlled within the specified range. If the air permeability is too large, the parachute cannot be fully inflated. If the air permeability is too small, the stability of the parachute is poor or even damaged. Fabrics used as carpets are required to have relatively high air permeability. Even if they are all fabrics for making clothes, their air permeability should also vary to ensure that the clothes are comfortable to wear. For example, summer clothes should have a large air permeability and good heat dissipation, while winter coats should have a small air permeability to improve the warmth retention effect. Therefore, appropriate air permeability is one of the prerequisites for fabrics to have good performance.


Test principle of fabric air permeability test


According to the specified method and parameters, clamp the sample at the air inlet of the fabric air permeability tester, and then adjust the fan speed to achieve a pressure difference on both sides of the fabric. The air permeability of the breathable fabric is determined based on the nozzle aperture and the size of the pressure difference on both sides. The air permeability refers to: the gas flow rate per unit area of the fabric vertically per unit time under the specified p.

Next, set a specified pressure difference on the tester, which is usually adjusted according to the test standard and fabric characteristics.

Then start the tester and measure the air flow through the fabric under the set pressure difference. The test results are expressed in volume flow units, such as cm's or L/min.

Finally, the tester automatically records the measured data and calculates the air permeability index of the fabric. According to different test standards, air permeability can be expressed as air flow or air permeability.

To ensure the accuracy and comparability of test results, various countries and regions have established multiple air permeability test standards. Common standards include the ASTM D737 standard of the American Society for Testing and Materials, the IS0 9237 standard of the International Organization for Standardization, and the Chinese national standard GBTT5453. These standards have detailed provisions for sample preparation, test conditions, data processing, etc. to ensure the scientificity and consistency of test results.


As a precision testing equipment, the automatic air permeability tester plays a vital role in testing the air permeability of textiles. Through scientific and rigorous testing methods, it can accurately evaluate the air permeability of fabrics and ensure product quality and effect. If you want to know more about this machine, please feel free to consult UTSTESTER.


Email: hello@utstesters.com

Direct: + 86 152 6060 5085

Tel: +86-596-7686689

Web: www.utstesters.com


Mechanisms, Testing, and Performance Analysis of Tear Strength in Textiles

2026-05-13

Introduction

Tearing is one of the most common forms of failure in textiles during actual use. Whether a jacket cuff gets caught on a tree branch, the knee of work pants is struck by a sharp object, or tent fabric is subjected to strong winds—these scenarios can all cause the fabric to tear rapidly along the yarn direction, starting from a localized notch.

Tear strength, as a core indicator for evaluating fabric durability and safety, directly impacts product lifespan and consumer safety. This article provides systematic technical guidance for textile testing laboratories by examining four key dimensions: failure mechanisms, testing methods, influencing factors, and instrument applications.


I. Physical Mechanisms of Tear Failure

1.1 The Nature of Tearing: Sequential Yarn Breakage

Unlike tensile failure, where an entire group of yarns bears the load simultaneously, tear failure exhibits significant stress concentration characteristics. When a notch exists at the fabric edge (e.g., a snag or cut), external force causes the yarns at the tip of the notch to first bear a load far exceeding the average. Once the first yarn breaks, the stress immediately transfers to the next yarn, creating a “domino-effect” chain of failures that ultimately results in rapid crack propagation.

During the tearing process, a characteristic stress triangle (Tearing Triangle) forms within the fabric:

- Vertex: The tip of the notch, where the single yarn currently breaking is located

- Base: The yarn system perpendicular to the tearing direction, which bears the primary load

- Hypotenuse: Adjacent yarns that are gradually drawn into the stress state


1.2 Factors Determining Tear Strength

Based on a mechanical analysis of fabric structure, tear strength primarily depends on the following factors:

1. Yarn tensile strength: Tear strength is directly proportional to the tensile strength of the yarn

2. Yarn elongation: The greater the elongation at break, the larger the area of the stress triangle, and the greater the number of yarns under stress, resulting in higher tear strength

3. Yarn coefficient of friction: Friction resistance between yarns affects stress transfer efficiency and the shape of the stress triangle

4. Fabric density and weave structure: Excessively high density may prevent yarns from sliding, thereby reducing tear strength


II. Testing Methodology and Interpretation of Standards

The most commonly used methods for testing fabric tear strength include the pendulum method (Elmendorf method), the tongue method (trouser method), and the trapezoidal method.

2.1 Pendulum Method (Elmendorf Method) — Dynamic Impact Test

Standards: GB/T 3917.1-2009, ISO 13937-1:2000, ASTM D1424-25

Test Principle: Based on the law of conservation of energy, the pendulum is raised to a predetermined height to acquire potential energy. Upon release, this potential energy is converted into kinetic energy to tear the specimen. By measuring the remaining swing angle of the pendulum after tearing the specimen, the energy consumed is calculated, thereby determining the tear strength.

Specimen Specifications: 63 mm × 100 mm rectangle with a 20 mm slit cut at the center

Scope of Application:

- ✓ Woven fabrics, nonwoven fabrics, laminated fabrics, pile fabrics, airbag fabrics

- ✓ Warp-knitted fabrics tested in the warp direction

- ✗ Weft-knitted fabrics, elastic fabrics, highly anisotropic fabrics

Technical Features:

- Fast testing speed (<1 second per test), simulating sudden tearing scenarios

- Force-time curve exhibits a typical sawtooth pattern, reflecting the process of a single yarn breaking

- Requires a multi-range pendulum (typically 200 gf–6400 gf); the test force should fall within 20%–80% of the range


2.2 Trouser Method (Single-Seam Method) — Constant-Speed Tensile Test

Standards: GB/T 3917.2-2009, ISO 13937-2:2000

Test Principle: A rectangular specimen is cut along the center of the short side to form a “trouser leg” shape. The two legs are clamped in the upper and lower grips of a tensile testing machine, respectively, and stretched at a constant rate (100 mm/min) while recording the force changes during the tearing process.

Data Collection Requirements: Divide the force-displacement curve into four equal segments. Discard the initial quarter and calculate the average of all peak values from the remaining three segments as the final result.

Differences from the Pendulum Method: The mechanisms of the two methods are similar, but the pant leg method involves slow, uniform tearing, whereas the pendulum method involves rapid impact tearing. For the same fabric, results from the pendulum method are typically slightly lower than those from the pant leg method.


2.3 Tongue Method (Double-Slit Method) — Bidirectional Tear Test

Standards: GB/T 3917.4-2009, ISO 13937-4:2000

Test Principle: Two parallel slits are cut into a rectangular specimen to form a tongue-shaped specimen. The tongues are clamped separately to keep the two cut lines parallel, and tensile force is applied along the cut lines to simulate a bidirectional tearing process.

Scope of Application: Widely used for various types of fabrics, including natural fibers, chemical fibers, and blended fabrics; particularly suitable for apparel fabrics and home textile products.


2.4 Trapezoidal Method — Multi-Yarn Synergistic Stress Test

Standards: GB/T 3917.3-2025 (New Edition), ASTM D5587

Test Principle: The specimen is cut into a trapezoidal shape with a central slit on the short side. The two non-parallel sides of the trapezoid are clamped, positioning the slit between the two jaws. During tensile testing, the tear propagates across the width of the specimen, causing a group of yarns to break sequentially under stress.

Technical Features:

- Unlike the single-yarn failure mechanism of the pendulum or single-tongue methods, the trapezoidal method exhibits multi-yarn cooperative tensile behavior

- Test values are typically significantly higher than those obtained by other methods (plain-weave cotton fabric: pendulum method < single-tongue method < double-tongue method < wing method < trapezoidal method)

- Suitable for thicker or high-strength fabrics, such as denim, industrial fabrics, and coated fabrics


2.5 Wing Method — Angular Variation Test

Standards: GB/T 3917.5-2009, ISO 13937-3:2000

Test Principle: Similar to the trapezoidal method, but the specimen is wing-shaped (isosceles triangle). By changing the clamping angle, the number of yarns subjected to force is adjusted.

Important Note: Although the wing-shaped method and the trapezoidal method belong to the same type of test, the test results cannot be directly compared due to differences in the angle of force application.


III. Guidelines for Selecting Test Methods

Principles for Method Selection:

1. Routine quality control: Give priority to the pendulum method (high efficiency) or the trapezoidal method (wide applicability).

2. Apparel products: The tongue method or pant method is recommended to simulate the forces encountered during actual wear.

3. Heavyweight/coated fabrics: The trapezoidal method must be used; the pendulum method may not be able to completely tear the fabric.

4. Arbitration Testing: Follow the method specified in the product standard; typically, the pant-shaped method or trapezoidal method is selected


IV. Key Factors Affecting Tear Strength

4.1 Raw Material Factors

Fiber Type: High-strength fibers (polyester, nylon) > natural fibers (cotton, wool). For fabrics of the same specification, the tear strength of polyester is typically 30–50% higher than that of cotton.

Yarn Structure:

- Plied yarn > Single yarn (twisting increases strength)

- Filament yarn > Staple fiber yarn (higher breaking strength)

- Textured yarn > Regular filament yarn (higher elongation, larger stress triangle)


4.2 Fabric Structure Factors

Fabric Density: There is an optimal density range. If density is too low, yarns are prone to slipping; if too high, yarns cannot slide to form stress triangles, which actually reduces tear strength.

Weave Structure:

- Plain weave < Twill weave < Satin weave (the fewer the interlacing points, the greater the yarn’s ability to slide)

- Knit fabrics typically have lower tear strength than woven fabrics (the loop structure is prone to deformation)

Post-processing Techniques:

- Resin finishing: Improves dimensional stability but reduces yarn slippage, resulting in a 20–40% decrease in tear strength

- Coating finishing: The coating penetrates yarn gaps, restricting yarn movement; evaluation requires the trapezoidal method

- Softening finishing: Increases yarn lubricity, promotes stress distribution, and can enhance tear strength


V. Industry Applications

Key Application Areas

Protective clothing: Firefighting suits and chemical protection suits require warp/weft tear strength ≥100 N (GB 24539-2021)

Outdoor gear: Tent and jacket fabrics must be evaluated for both tear strength and seam performance

Industrial Textiles: Geotextiles and filtration materials are evaluated using the trapezoidal method, with a requirement of ≥250 N (GB/T 17634)

Automotive Interiors: Airbag fabrics are tested using the pendulum method, with a requirement of ≥200 N in both warp and weft directions (ISO 13937-1)


Conclusion

Textile tear strength testing is a comprehensive discipline involving materials mechanics, structural engineering, and standardization technology. From the rapid impact of the pendulum method to the multi-yarn interaction of the trapezoidal method, different testing methods reveal distinct mechanisms by which fabrics resist tearing.

If you require technical consultation regarding specific fabric types or testing methods, please contact the UTSTESTER technical team for customized solutions.


Email: hello@utstesters.com

Direct: + 86 152 6060 5085

Tel: +86-596-7686689

Web: www.utstesters.com


Analysis of Factors Affecting Fabric Water Vapor Permeability

2026-05-09

I. What Is Fabric Water Vapor Permeability?


Fabric water vapor permeability refers to a fabric’s ability to allow water vapor to pass through it, and it is one of the core indicators for evaluating the comfort of functional textiles. During physical activity, the skin continuously evaporates moisture (sweat). If the fabric cannot promptly expel this water vapor, a hot and humid microenvironment will form on the skin’s surface, leading to discomfort.


Water vapor permeability and water repellency together constitute the dual standards of “breathability” and “protection” for outdoor functional apparel. An excellent piece of functional apparel must both block the intrusion of external liquid water and rapidly expel water vapor from the body—this is precisely where the value of water vapor permeability research lies.


II. Testing Methods for Water Vapor Permeability


1. Desiccant Method (Positive Cup Method)

Standards: GB/T 12704.1, ASTM E96, JIS L1099 A-1

Principle: A desiccant (anhydrous calcium chloride) is placed in a moisture permeability cup, and the test sample is sealed at the cup opening. After being kept in a constant temperature and humidity environment for a specified period, the moisture permeability is calculated by measuring the weight gain of the desiccant.

Features: The test conditions are mild and closely resemble actual wearing conditions, making it the most commonly used testing method in China.


2. Evaporation Method (Water Method, Inverted Cup Method)

Standards: GB/T 12704.2, ASTM E96 BW, JIS L1099 B-1

Principle: A specific volume of distilled water is placed in a moisture transmission cup. After sealing the sample, the cup is inverted. Water vapor passes through the sample and evaporates outward; the moisture transmission rate is calculated by measuring the decrease in water mass within the cup.

Features: Testing conditions are relatively harsh, simulating a high-humidity environment, making it suitable for waterproof and breathable fabrics.


3. Sweating Guarded Hotplate Method

Standards: ISO 11092, GB/T 11048

Principle: A porous metal plate is used to simulate skin perspiration. The energy required to maintain a constant temperature is measured, directly yielding the fabric’s moisture resistance (Ret) and water vapor transmission index (imt).

Features: This method more closely approximates actual human physiological conditions and is considered the “gold standard” for evaluating thermal and moisture comfort.


III. Key Factors Affecting the Moisture Permeability of Fabrics


(Ⅰ) Fiber Raw Material Factors


1. Moisture Absorption of Fibers

The moisture absorption of fibers is the foundation for determining moisture permeability. Based on how fibers interact with water, they can be classified as follows:


- Hydrophilic fibers: cotton, viscose, wool, silk, etc. The molecular structure of these fibers contains hydrophilic groups (-OH, -COOH, -NH₂), which can adsorb water molecules via hydrogen bonding and transport them through diffusion within the fiber. Fibers with strong moisture absorption typically exhibit better moisture vapor permeability.

- Hydrophobic fibers: Synthetic fibers such as polyester, nylon, and polypropylene. These fibers do not absorb water themselves; water vapor is primarily transported through the pores in the gaps between fibers. Although the moisture vapor transmission capacity of a single fiber is limited, excellent moisture vapor transmission performance can be achieved through specialized structural designs.


2. Fiber Fineness and Cross-Section Shape


- Fiber fineness: The finer the fiber, the larger the specific surface area, and the more dense the capillary network formed between fibers, which facilitates the conduction of water vapor. Fabrics made from ultra-fine fibers (<0.5 dtex) typically exhibit superior moisture vapor transmission performance.

- Cross-sectional Shape: Fibers with non-circular cross-sections (such as cross-shaped, trefoil-shaped, or hollow fibers) can form more pore channels compared to circular fibers, thereby increasing the pathways for water vapor transmission. For example, hollow polyester fibers not only reduce weight but also significantly enhance moisture permeability and thermal insulation.


(II) Yarn Structure Factors


1. Yarn Twist

Twist directly affects the density and porosity of the yarn:


- Low-twist yarn: The yarn is loose, with large gaps between fibers, resulting in low resistance to water vapor transmission and good moisture permeability. However, the yarn has lower strength and reduced abrasion resistance.

- High-twist yarn: The yarn is compact, with reduced gaps between fibers, leading to increased resistance to water vapor transmission and reduced moisture permeability. However, the yarn has high strength, and the fabric feels stiff and crisp.


2. Yarn Blend Ratios


- Cotton/Polyester Blends: Cotton fibers provide moisture absorption and wicking capabilities, while polyester provides strength and quick-drying properties. When the cotton content is between 40% and 60%, moisture permeability and durability achieve a good balance.

- Wool/Nylon Blends: The natural moisture-absorbing properties of wool combined with the strength of nylon are commonly used in high-end outdoor apparel.


(III) Fabric Structure Factors


1. Fabric Density and Tightness


- Increased Density: Warp and weft yarns are arranged more tightly, reducing fabric porosity, increasing resistance to water vapor transmission, and lowering moisture permeability.

- Decreased density: Fabric porosity increases, improving moisture vapor permeability, but this may lead to reduced wind resistance and insufficient strength.


2. Fabric Thickness

Fabric thickness is inversely correlated with moisture vapor permeability: the diffusion resistance that water vapor must overcome to pass through the fabric is directly proportional to its thickness.


3. Weave Structure

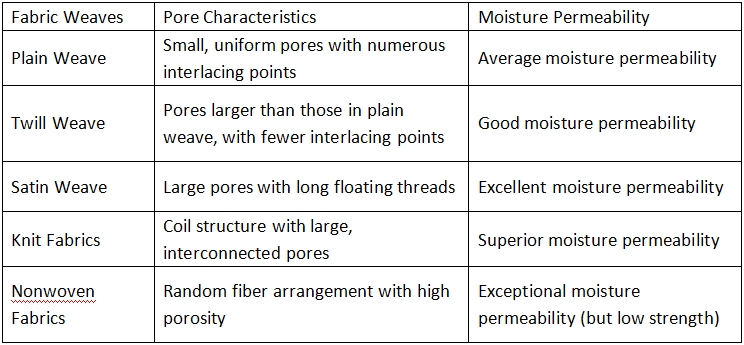
The pore morphology formed by different weave structures varies significantly:

4. Multi-layer Composite Structures

Modern functional apparel often employs multi-layer composite designs:


- Two-layer fabrics: The outer layer is windproof and waterproof, while the inner layer wicks away moisture and sweat; the “pump effect” created by the pores between the layers enhances moisture vapor permeability.

- Three-layer composites: Fabric + waterproof and breathable membrane + lining. The membrane’s microporous structure allows water vapor molecules to pass through while blocking liquid water.


(IV) Post-processing Factors


1. Coating Treatments

Coating is a key method for modifying moisture vapor permeability:


- PU Coating: Standard PU coatings block fabric pores, significantly reducing moisture vapor permeability. However, microporous PU or hydrophilic PU coatings can maintain a certain level of moisture vapor permeability while retaining waterproofing properties.

- Microporous PTFE Membrane: Features extremely high porosity and very small pore sizes, offering high moisture vapor transmission rates and water pressure resistance.

- Non-porous hydrophilic membranes: These utilize a “adsorption-diffusion-desorption” moisture transmission mechanism via hydrophilic groups on the molecular chains. While their moisture permeability is slightly lower than that of microporous membranes, they offer better wash resistance.


2. Water-repellent and moisture-permeable finishing agents

- Fluorocarbon compounds: These impart water- and oil-repellent properties to fabrics but have a certain negative impact on moisture permeability.

- Silicone-based compounds: Form a breathable film on the fiber surface, with minimal impact on moisture permeability.

- Nanotechnology treatments: Such as nano-SiO₂ and TiO₂, which impart special functions while maintaining porosity.


3. Moisture-Wicking Finishes

Treating hydrophobic synthetic fiber fabrics with hydrophilic finishing agents (such as polyether-based or polyacrylic-based compounds):


- The finishing agents form a hydrophilic layer on the fiber surface, improving surface wettability.

- A wicking effect is created, rapidly transporting sweat from the skin side to the outer layer for evaporation.

- Moisture vapor transmission can be increased by 20%–40%, while maintaining the quick-drying properties of synthetic fibers.


(V) Environmental Factors


Both moisture vapor transmission testing and actual use are significantly influenced by environmental conditions:


1. Temperature

- Rising temperature: The kinetic energy of water vapor molecules increases, accelerating diffusion; simultaneously, fibers expand after absorbing moisture, enlarging their pores. Moisture vapor transmission rate increases significantly with rising temperature.


2. Relative Humidity

- High-humidity environment: The concentration gradient of water vapor on both sides of the sample decreases, reducing the driving force and lowering the moisture vapor transmission rate.

- Low-humidity environments: The concentration difference is large, resulting in high moisture vapor transmission rates.

- Isothermal and isohygric conditions: When the temperature and humidity on both sides of the sample are identical, the moisture vapor transmission rate is zero.


3. Wind Speed

- Increased wind speed accelerates the loss of water vapor from the sample’s surface, maintaining a higher concentration gradient and thereby increasing the moisture vapor transmission rate.

- In actual outdoor wear, wind speed is a key variable affecting perceived comfort.


IV. Balancing Moisture Permeability with Other Functions


1. Moisture Permeability vs. Water Resistance

Conflict: Water resistance requires extremely small or closed fabric pores, while moisture permeability requires open pores.

Solutions: Microporous membrane technology, hydrophilic non-porous membranes, and high-density weaving techniques (such as high-density fabrics made from ultra-fine fibers).


2. Moisture Permeability vs. Windproofing

Conflict: Windproofing requires a tightly woven fabric structure, while moisture permeability requires unobstructed pores.

Solutions: Multi-layer composite structures, membrane technology, and adding a windproof fabric layer on the outer side of the moisture-permeable membrane.


3. Moisture Permeability vs. Thermal Insulation

Conflict: Thermal insulation requires a layer of still air (loose structure), but excessive thickness reduces moisture permeability.

Solutions: Hollow fibers, 3D knitted structures, and phase-change materials for temperature regulation.


Conclusion


Fabric moisture vapor permeability is a complex system involving multiple interacting factors, spanning disciplines such as fiber science, textile engineering, polymer materials, and heat and moisture transfer.

UTSTESTER provides precise moisture vapor permeability testing equipment. If you encounter any issues during moisture vapor permeability testing, please feel free to contact our technical team at any time.
Water Vapour Permeability Tester


Email: hello@utstesters.com

Direct: + 86 152 6060 5085

Tel: +86-596-7686689

Web: www.utstesters.com

F-SP Pro Series Swimming Pool Pumps A High-Efficiency Variable Frequency Solution for Modern Pool Circulation Systems

2026-04-29

In today’s pool circulation systems, energy efficiency, operational stability, and intelligent control are no longer optional—they are essential. Traditional fixed-speed pool pumps are increasingly being replaced by variable frequency (VFD) pool pumps, which significantly reduce energy consumption while improving system adaptability.


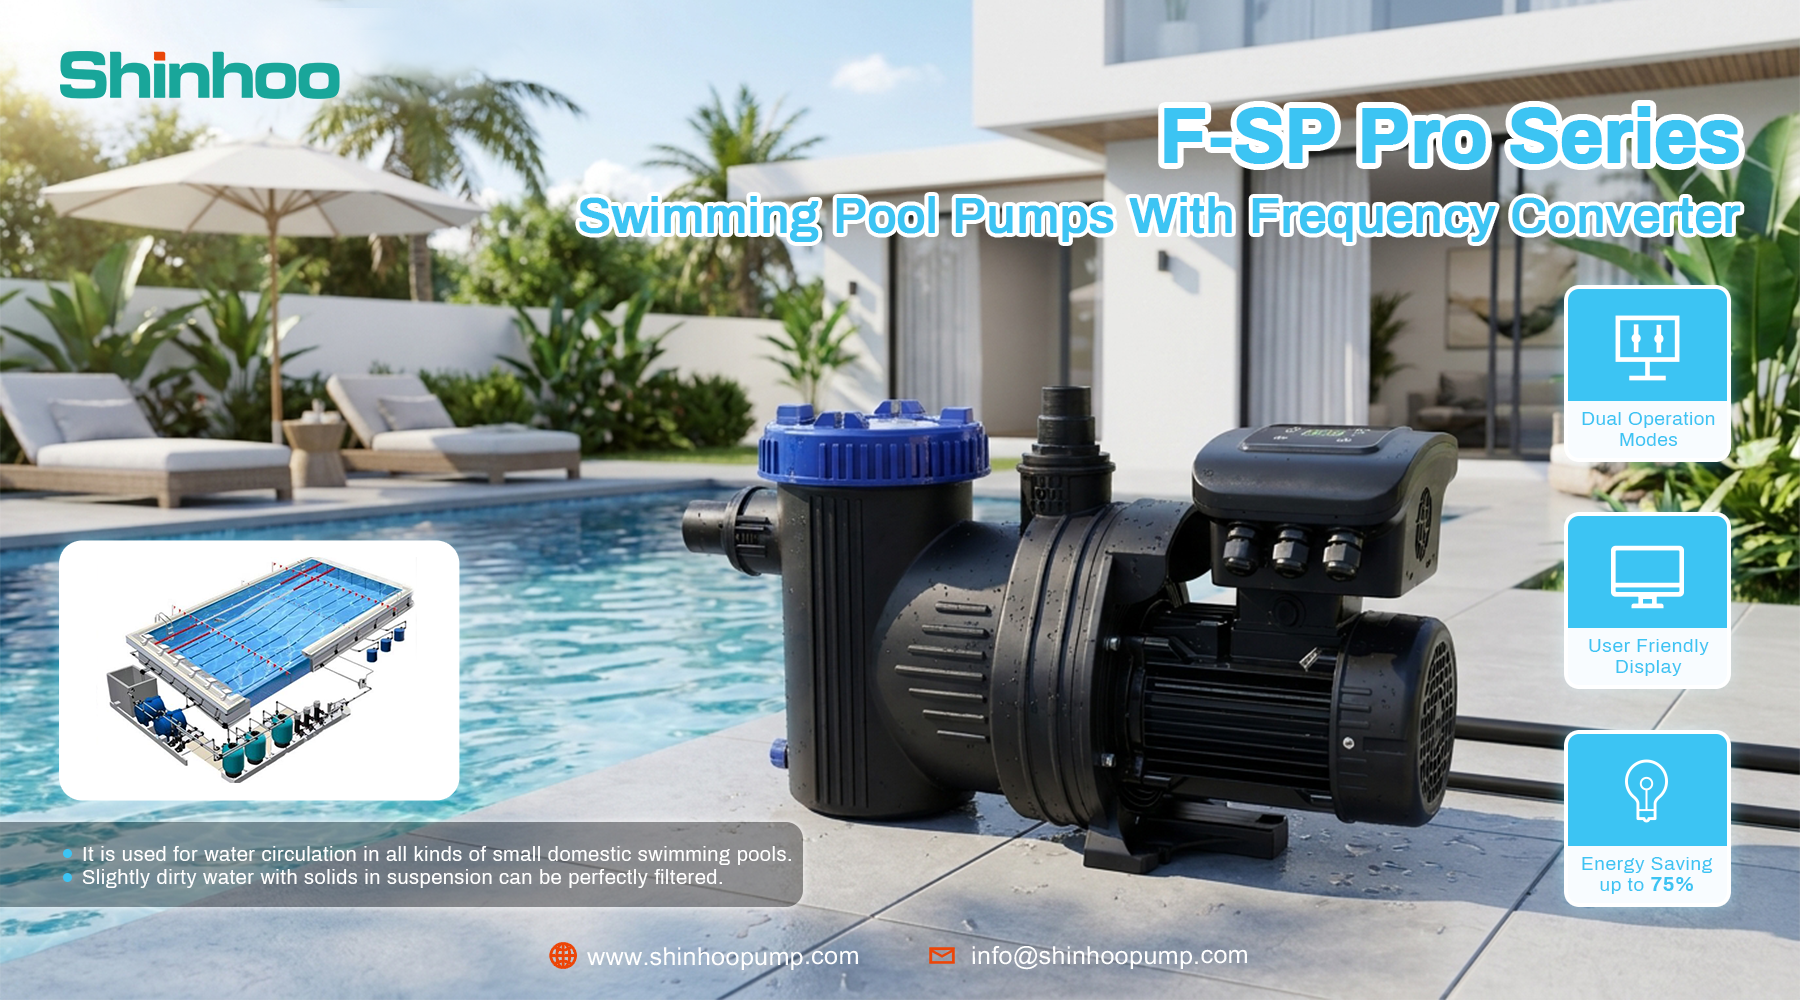
The F-SP Pro Series Swimming Pool Pump with Frequency Converter is engineered to meet these evolving demands, offering a balance of performance, filtration capability, and intelligent control tailored for small to medium-sized residential pools.


What Makes the F-SP Pro Series Stand Out

The F-SP Pro Series integrates a high-efficiency hydraulic design with an embedded frequency converter, allowing dynamic speed adjustment based on system demand.

· Integrated Frequency Converter (VFD) 

· Dual Operation Modes 

· User-Friendly Digital Interface 

· Energy Savings up to 75% 

· Optimized for Slightly Dirty Water Conditions 

Unlike conventional pumps, this system is designed not just for circulation—but for intelligent water management.


Typical Use Cases:

· Residential swimming pools

· Small commercial pools

· Initial filtration stages

· Pools with moderate debris load

F-SP Pro Series

The F-SP Pro Series is more than just a circulation pump—it represents a shift toward intelligent, energy-efficient pool management systems.

High-Efficiency Pump for Heat Pumps & HVAC Systems – Shinhoo Grand 25-23 Pro

2026-04-29

For heat pump systems, underfloor heating mixing stations, and HVAC integrators, pump efficiency, control accuracy, and refrigerant compatibility are critical to system performance and regulatory compliance. The Shinhoo Grand 25-23 Pro – a permanent magnet variable frequency pump – delivers ultra low energy consumption, precise flow feedback, and an A3 explosion proof rating. It provides a safe, high efficiency circulation solution for systems using R290 and other eco friendly refrigerants.Grand 25-23 Pro

IE5 Efficiency – EEI ≤ 0.23

The Grand 25-23 Pro achieves an EEI value as low as 0.23 (Part 2), far exceeding EU energy efficiency standards. Its high efficiency permanent magnet motor offers:

l Rated flow: 8 m³/h

l Rated head: 12.5 m

l Max. flow: 14 m³/h

l Max. head: 23 m

While delivering strong hydraulic performance, the pump minimizes energy consumption – helping systems earn green building certifications and meet low carbon operation targets.

Multiple Control Modes – Flexible Adaptation

The pump supports constant speed, constant pressure, proportional pressure, AUTO, and PWM control modes, easily adapting to different operating conditions. Whether in constant flow or variable flow systems, it delivers precise adjustment and avoids unnecessary energy waste.

High Accuracy Flow Feedback – Stable & Reliable

Flow feedback accuracy reaches ±0.2 m³/h, providing dependable data for system monitoring and optimization. Combined with IP44 protection, the pump ensures long term stable operation even in humid or mildly dusty environments.

A3 Explosion Proof – R290 Refrigerant Compatible

Certified with an A3 explosion proof rating, the Grand 25-23 Pro is specifically designed for systems using flammable eco friendly refrigerants such as R290. It meets safety requirements for heat pumps, chillers, and refrigeration equipment – helping customers address increasingly stringent environmental and safety regulations.


Global Certifications – Proven Quality

The pump holds CCC, TUV, CE, EMC, ROHS, and REACH certifications, confirming electrical safety, electromagnetic compatibility, and material environmental compliance. System integrators can specify the pump with confidence, shortening compliance review cycles.

Typical Applications

l Heat pump systems (air source / water source heat pumps)

l Underfloor heating mixing stations

l Domestic hot water circulation

l HVAC terminal circulation


Why Choose the Shinhoo Grand 25-23 Pro?

The Shinhoo Grand 25-23 Pro combines ultra low energy consumption, precise control, refrigerant compatibility, and robust quality – offering a highly efficient, safe, and compliant pumping solution for modern heat pump and HVAC systems. Lower your operating costs and strengthen system competitiveness – choose the Grand 25-23 Pro for your next project.

Tags
#vs